Tuesday, 5 March 2013

The Second Sword


This sword is the brother to the one shown here some time ago in every sense, made from the same antique metal, made by the same method and the same hand. 
 
They are also a pair in their purpose as symbols of dedication, heritage and protection to be exchanged between Bride and Groom.

So, the piece in question was begun in this way,  a stack is welded together and folded a dozen times to create a unique, new piece of steel that aims for homogeneity but achieves the lustrous, patterned metal that enticed our ancestors.
 
Loud Video!


This folded steel is then drawn out into a long bar and divided in two.
Between these two pieces a new piece of low carbon mild steel is forge welded in, forming a “core” to the blade.
 
This is now ready to be forged into the form of the sword, with its important central groove or fuller being forged in, as not to compromise the outer steel and reveal the soft steel core.


The Tang was forge welded on separately. This method was widely used in the past.
 
At this final stage, I noticed some cracks at the tip of the sword, and on closer inspection it seemed likely that I had overheated this part of the blade during the forge welding. This presented a quandary as I did not want to start the blade again due to the significance held with both swords being made from the same steel, but I also could not satisfactorily finish and deliver a sword with such flaws.

So it became clear to me that I needed to repair this sword.

Many ancient blades exhibit evidence of having been reforged or welded at some point during their life. The sagas tell us that breakages were a fairly common outcome of sword fighting and craftsman of the day had to repair those blades deemed too valuable to simply discard as broken.

This is quite an achievement as a sword that breaks in use is a sword that has been finished, has been ground and polished and is thus- thin. Too thin perhaps for most smiths of any era to confidently re- forge weld flawlessly to condition that the blade can be re-hardened, re- polished and returned to use. But, this they did.

With this is mind I began preparing for the repair which firstly involved making more folded steel.

The damaged area of the tip was cut off and the folded steel was forged and divided into two pieces, each piece being carefully formed to the tapering shape of the new tip.


The new steel was welded very carefully as a single misplaced hammer blow would leave an impression beyond what could be removed with careful grinding and polishing.

 
This was perhaps the most intense 20 minutes of forging I have ever done and I am proud to say that the result was a flawless weld that is as strong, if not stronger than the rest of the sword.

The fact that this area welded so well can be seen in the final polish and etch of the blade, where the decorative grain of the sword suddenly changes to the new steel. The contrast has to be looked for to be found but is an element of detail unique to the life story of this blade and I feel adds to the sense of history this sword.


Careful etching reveals the subtle character of the steel.

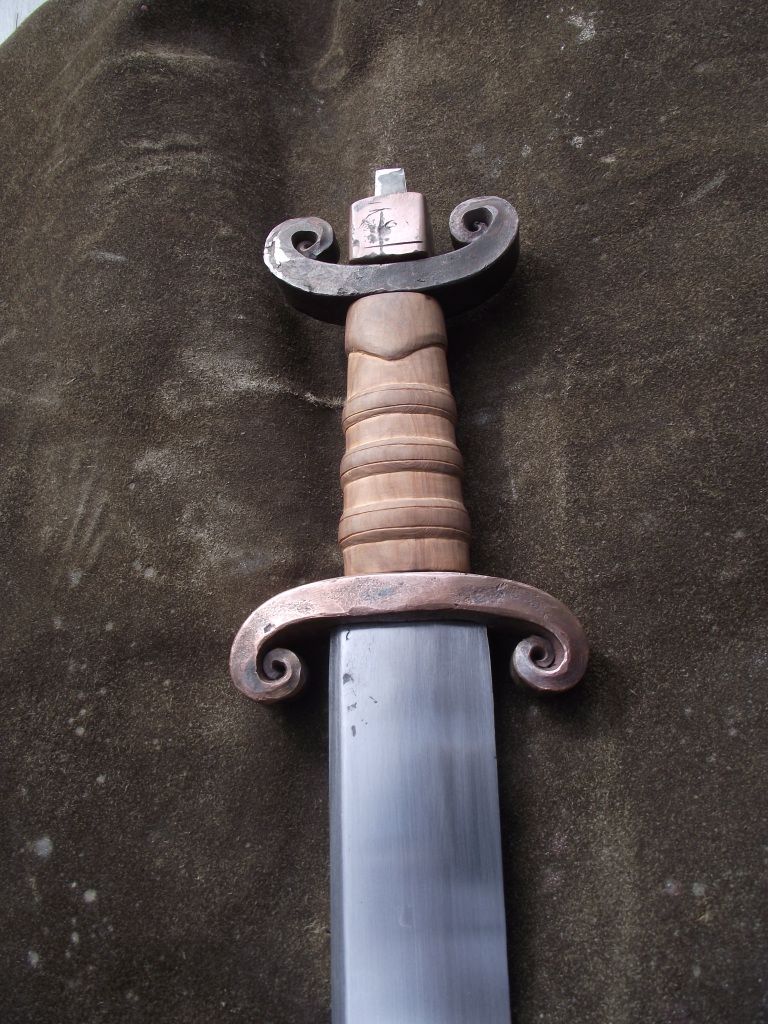
The hilt on this sword was a lot more intricate and involved than the hilt parts of the first sword. The pommel is loosely inspired by type B as if tapers in two directions. The rough form was forged and hot punched with a drift that was the clone of the tang, ensuring a tight fit with no need for fettling.


The top and bottom guard were to be overlaid with brass and copper. This challenging technique was very popular form of hilt embellishment for centuries and involves the careful preparation of hundreds of grooves, undercut and inlaid with wire. The wire is then planished (hammered with a small hammer with a polished face) this method spreads the wires until they butt up against each other.


Eventually, the entire surface of the guards was covered in this way.

To commemorate the repair or healing of this blade I inlayed this symbol into the pommel.


A wooden core was made from Pear wood, this will be wrapped with brass wire to add another layer of detail and decoration.
 

The power of these objects can only really felt when there seen together, as a pair.


As whole as these look, they aren’t yet fixed together. The peening of the tang is left to the very last moment to allow for small adjustments. When this final act has been finished, the swords are together, one object made from many pieces. They come to life at this point their balance is final and they finally feel like a sword.


Monday, 4 February 2013

Winter Work


Busy weeks have gone by since my last update.
 
 I have made several axes, forged a Sword from my own folded steel, begun a composite pattern welded bowie knife as well as begun and finished some architectural commissions with my Father.


I would like to show some of father’s recent pieces before showing mine.
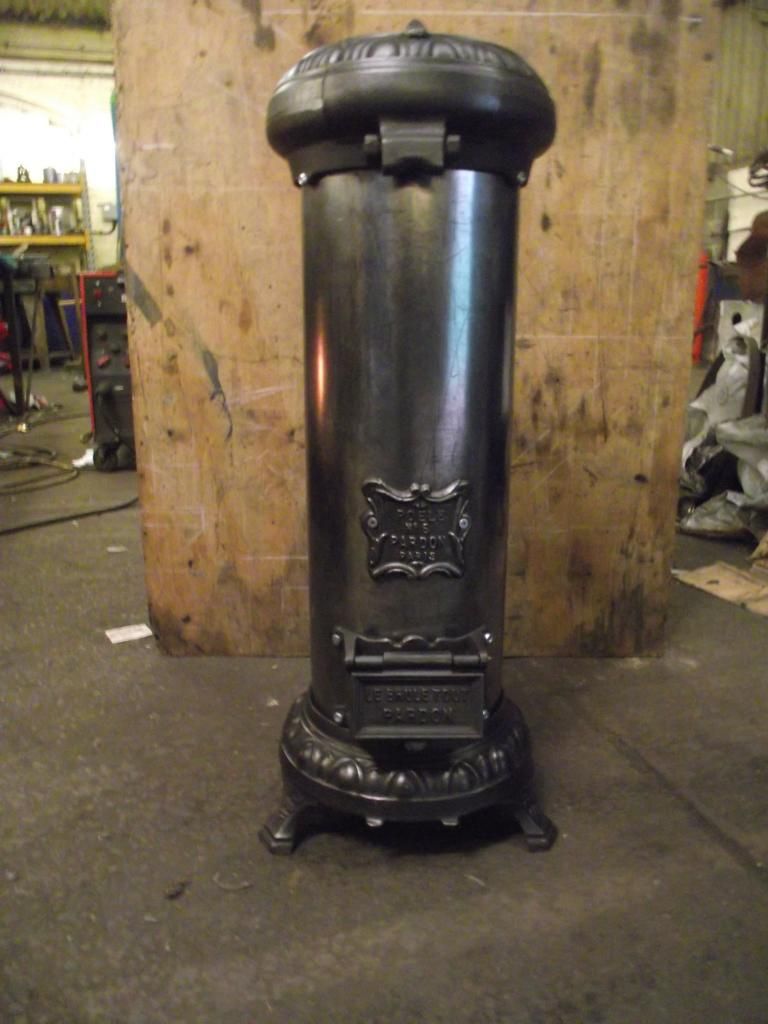
Firstly this antique, French made charcoal burning stove we restored from a ruined and rusty state. We had to make the three feet by 12” cylinder by hand to fit the allocated slots in the casting.  The Castings were decorated with laurel leaves and olives. It was a pretty thing and now will function for another century to come.
 
 
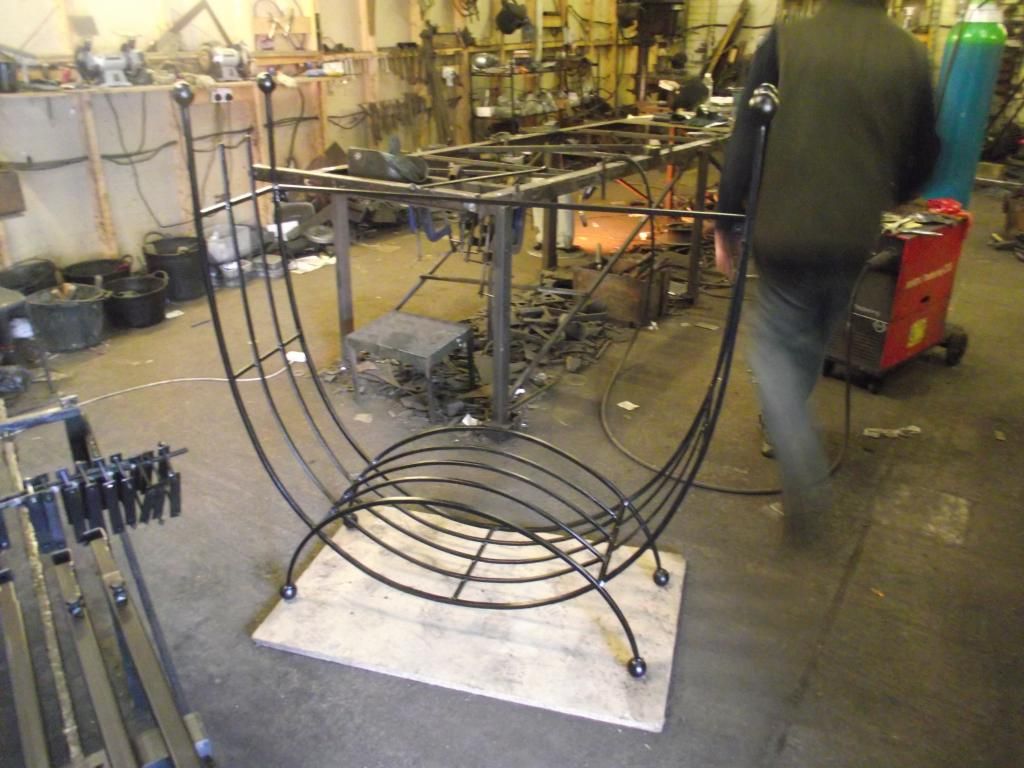
Another example of what my Dad has made recently is this large log basket with an understory for kindling.
Four feet tall and three and a half feet wide.


______________________________________________________________________________
 
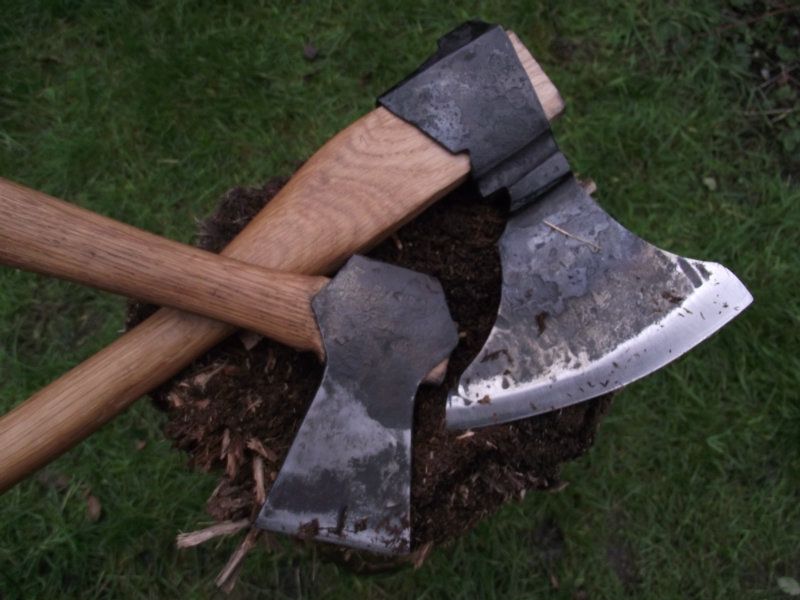
I’ve continued my work into axes for wood working producing a few hatchets based on the full “bowtie” method used in the past.  


To be honest, I am very proud of these axes. The technique allows for a tremendous variety in design whilst remaining thoroughly rooted in tradition. Tradition is truth when it comes to tool making. After years of working in craft from timber framing to jewellery to decorative ironwork, I have found repeatedly the tried and tested tools and methods are by far and away the most ergonomic, efficient and beautifully ways to achieve our goals.

  The method in question here, the “bowtie”, creates a thick, strong poll which adds beautiful balance and heft. The method of drawing out the cheeks is a joy to me. The form of these axes can be entirely achieved by hand forging with little to no amendments with a file or grinder. In this sense it is, to me, pure.

These hatchet heads weigh 1.5lbs each and are available, made to order.  Another advantage to this symmetrical design is their ambidexterity, as they simply need to be hafted from either side for use with the left or right hand.
 Hafting in this case has been done with English oak we reclaimed from a building site some months ago.  The hafts were initially axe- hewn then draw-knifed and filed and scraped down for a smart finish. The eye was fitted tightly before the slot was sawn and a fitted with a solid walnut wedge.

 
At all times when producing tool handles, effort must be taken to observe the grain flow of the timber used, ensuring correct orientation for maximum strength and durability. Whilst there are certainly some woods that are unsuitable for hafting, many species that are over looked by larger tool and axe manufacturers are more than adequate for smaller axe types- particularly those axes that are used sensitively for specialised purposes such as carving and hewing.

Axes are a passion for me because their making involves such elegant process. If I can produce an axe for you, it would make me very happy.

Saturday, 12 January 2013

Socketed Side Axe


I have been thinking about traditional forms of the axe used in timber framing and log building, one of the quintessential types is the “Side-Axe”, so called because it allows the user to stand to the side of the timber or beam and hew without having to use the tool awkwardly as the bit (blade) is orientated at an angle to the shaft.

Many of the older style of axes are exciting works of iron that show millennia of evolution and improvements to design. There are other methods of production that I want explore that involve many delicate process’. The most important thing to understand about the design of older axes is that they are made of Wrought Iron, not steel and as such the grain flow of the material needs to be considered before an axe can be made.

I’ve made this axe using an altered form of the asymmetric wrap that Jim Austin has been exploring in his research on Viking methods of construction; my own research has shown that this technique was widely used in axe manufacture until the modern age and the advent of homogenised, low to zero slag alloys which can be worked more directly with punching and drifting methods as the material wont splits apart under these stresses.
 
This image shows an excavated Early modern broad axe with an exploded asymetric wrap on the eye. I have taken this image from the Portable Antiquities Scheme website.


The stock I began with was around 5 feet of 20x 50 mild steel, the end of which was upset on a block on the floor to thicken the stock further in anticipation of the forming a wide Bit later on as the axe I have made is also of the “broad-axe” family having and edge length just over 6 inches.

Upsetting is done whilst the stock is still long and very heavy to allow more force to be delivered in each strike.

(Apologies, I have no video editing skills or software so all of my films are Very loud! But then again, so is my work…. You have been warned!)  


Seven inches are measured and then chopped off and marked up with a centre punch.


I also forged this tool, called a butcher, to help making the early defining cuts.
 
 
The Butcher is a hafted top set normally struck by a helper with a sledge but can be used by the smith if the work is held between the legs.


A series of fullers and flatters are used to pull the steel in the desired direction.


This is neatened up over my stake Anvil which has sharper edges

This neatened piece is measured to check symmetry and then folded over and welded onto itself. The faces that are welded to each other are over thick to allow multiple welding passes to ensure a thorough bond.


Before the weld is completed, the axe is held vertically and the butcher is used again to fiercely cut through the weld I have just set, this pushes the mass of the axe forward but also upsets the area of the weld, thickening it again so it can be gently worked at welding temp to finish.


Once the eye had been mostly welded, the eye was trued up with a large tapering square mandrill.

Square eyes are more common on older styles of working axe and in my opinion allow for simpler fitting of a haft.


Finaly the high carbon edge was inserted and welded in, the form was forged out with fullers and flatters and left to normalise before being rough ground and hardened.


The head was ground on the reverse side and the black scale was treated with beeswax to protect against rust.


This axe head is for sale
 
I am making some more working axes in the coming weeks as well as some more decorative and embellished styles using a range of techniques. I am available to make specialist axes of any kind, please contact me either here or though my Facebook page here-